
A comprehensive technical analysis of variable frequency drive-induced bearing failures and the critical role of properly screened medium-voltage cables in harsh industrial environments
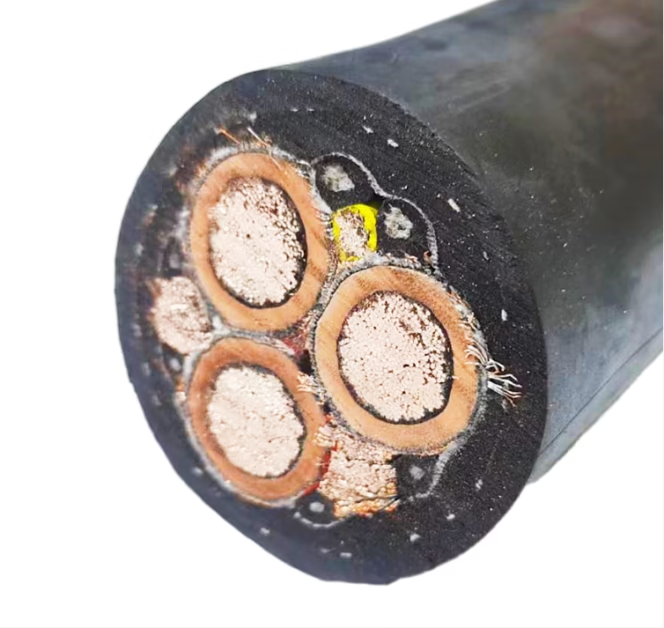
VFD Motor Bearing Damage: Why You Need (N)3GHSSYCY Screened Mining Cables?
A comprehensive technical analysis of variable frequency drive-induced bearing failures and the critical role of properly screened medium-voltage cables in harsh industrial environments
Understanding the Critical Problem
了解关键问题
Variable frequency drives (VFDs) have revolutionized industrial motor control by enabling precise speed regulation and significant energy savings. However, these benefits come with a serious technical challenge that many facilities overlook until catastrophic failure occurs. When VFDs control AC motors through pulse width modulation (PWM), they create high-frequency electrical disturbances that can destroy motor bearings in a matter of months or even weeks, rather than the expected operational lifetime of years.
The mechanism behind this premature failure is well-documented in engineering literature. VFD output uses direct current pulses to induce motor motion, and these pulses cause interference with electrical signals through the motor and motor cables. The problem stems from the fact that VFD transistors convert pure sine wave power into a series of positive and negative pulses. Unlike balanced three-phase power where voltages cancel each other out, VFD-generated waveforms create common mode voltages that induce shaft voltages in the motor.
Critical Failure Timeline
According to industry research, motors controlled by VFDs can experience complete bearing failure within remarkably short timeframes. Most motor bearings are engineered for approximately 100,000 hours of operation, yet VFD-controlled motors frequently fail within 720 hours (one month) of operation. In documented cases from pulp and paper facilities, VFD-controlled motors typically failed due to bearing damage within six months of installation.
Source: Pumps & Systems – “Preventing Drive Induced Electrical Damage to AC Motor Bearings” https://www.pumpsandsystems.com/preventing-drive-induced-electrical-damage-ac-motor-bearings
Technical Mechanism of VFD-Induced Bearing Damage
VFD引起的轴承损坏的技术机制
Capacitive Discharge Currents
When VFDs operate, the rapid voltage switching creates capacitive coupling between motor windings, the stator, the rotor shaft, and the motor frame. This capacitance stores electrical charge on the motor shaft. When the shaft voltage builds up sufficiently to overcome the dielectric properties of the bearing grease, it discharges through the bearing in the form of electrical arcs. These discharges occur during virtually every VFD cycle, creating millions of tiny electrical arcs per hour through the bearing surfaces.
High-Frequency Circulating Currents
A second destructive mechanism involves high-frequency (HF) circulating currents that result from magnetic flux produced by common mode current flowing in the motor phases. In properly balanced three-phase power, common mode current equals zero. However, VFD operation ensures that common mode current is never zero, creating continuous circulating currents that flow from the motor frame through the bearings to the shaft and back to ground. Larger motors generally experience more severe damage from these circulating currents.
| Damage Mechanism 损坏机制 | Technical Cause 技术原因 | Primary Effect 主要影响 | Failure Timeline 故障时间线 |
|---|---|---|---|
| Capacitive Discharge (EDM) 电容放电 | Shaft voltage buildup from capacitive coupling 电容耦合引起的轴电压积聚 | Bearing surface pitting and frosting 轴承表面点蚀和磨砂 | 3-6 months |
| HF Circulating Current 高频循环电流 | Common mode voltage in unbalanced phases 不平衡相位中的共模电压 | Accelerated bearing race degradation 加速轴承座圈退化 | 1-3 months |
| Bearing Fluting 轴承槽纹 | Accumulated pitting creating washboard patterns 累积点蚀形成波纹图案 | Excessive vibration and noise 过度振动和噪音 | 6-12 months |
| Insulation Breakdown 绝缘击穿 | Voltage spikes exceeding insulation rating 电压尖峰超过绝缘额定值 | Motor winding short circuits 电机绕组短路 | 2-4 months |
Source: EST AEGIS – “How Do VFDs Cause Bearing Damage?” https://blog.est-aegis.com/how-do-vfds-cause-bearing-damage
Electrical Discharge Machining (EDM) in Bearings
The electrical arcing through bearings is fundamentally identical to electrical discharge machining (EDM), an industrial process used to remove metal through controlled electrical discharges. Each arc creates a small molten crater on the bearing surface where it strikes. As these pits accumulate over thousands of operating hours (or in VFD applications, often just hundreds of hours), they create a characteristic “frosted” appearance visible under microscopic examination. This frosting eventually progresses to fluting, which appears as washboard-like ridges across the bearing race. The resulting friction increase leads to noise, further grease deterioration, and ultimately complete bearing failure.
Source: Motion Control Tips – “Problems VFDs Cause and Cable Types That Help Solve Them” https://www.motioncontroltips.com/problems-vfds-cause-cable-types-help-solve/
The Critical Role of Screened VFD Cables
屏蔽VFD电缆的关键作用
Proper cable selection represents one of the most effective and economically viable solutions to VFD-induced bearing damage. Standard power cables were designed for sinusoidal AC power and lack the specialized construction necessary to handle the harsh electrical environment created by VFD operation. The rapid voltage rise times (dv/dt) produced by modern insulated gate bipolar transistors (IGBTs) create electromagnetic interference (EMI) and common-mode noise that unshielded cables cannot adequately contain.
Why Standard Cables Fail in VFD Applications
On a conventional 60 Hz utility grid, voltage transitions from zero to peak voltage occur over approximately 4 milliseconds, producing a rise time of less than 1 volt per microsecond. In contrast, VFD output voltage transitions from zero to full DC bus voltage (typically 650V for 480V motors) in approximately one microsecond. IGBT output devices typically switch at rates between 1,200 and 5,000 times per cycle, depending on drive switching frequency settings. This creates square-wave amplitude that remains at full DC bus voltage even at low motor speeds.
Standard cables using PVC insulation and lacking proper shielding create several problems in this environment. The capacitance of unshielded cables allows common-mode currents to flow through unintended paths, including through motor bearings to ground. Metal conduit or cable trays containing unshielded cables can conduct EMI and common-mode noise to the nearest earth ground, creating destructive ground loops. Without proper shielding connected at both the drive and motor ends, high-frequency noise has no controlled path back to the drive, forcing it through bearings and other sensitive components.
| Cable Parameter 电缆参数 | Standard Cable 标准电缆 | VFD-Rated Cable VFD额定电缆 | Screened Mining Cable 屏蔽矿用电缆 |
|---|---|---|---|
| Insulation Type 绝缘类型 | PVC (15-20 mil) | XLPE (20+ mil) | EPR Type 3GI3 |
| Corona Inception Voltage 电晕起始电压 | < 800V | > 1200V | > 1500V |
| Shielding Configuration 屏蔽配置 | None or minimal | Foil + braided mesh | Multi-layer with monitoring |
| Ground Path 接地路径 | Single conductor | 3 symmetrical grounds | Spiral copper + armor braid |
| Mechanical Protection 机械保护 | Minimal | Moderate | Steel wire braid armor |
Source: Quad Plus – “Why Do I Need Special VFD Cable” https://quadplus.com/vfd-special-cables/
(N)3GHSSYCY Screened Mining Cable Specification
(N)3GHSSYCY屏蔽矿用电缆规格
The (N)3GHSSYCY cable designation represents a medium-voltage screened flexible cable specifically engineered for the most demanding industrial applications, particularly in mining and tunneling environments where VFD-controlled equipment operates under extreme mechanical and electrical stress. This cable construction follows the rigorous requirements of DIN VDE 0250 Part 605, the German standard for screened flexible cables with rubber insulation and PVC sheath for nominal voltages of 3.6/6 kV and 6/10 kV.
Construction Details and Technical Specifications
The cable employs flexible stranded copper conductors manufactured to Class 5 specification according to DIN VDE 0295, ensuring maximum flexibility for mobile equipment applications. The insulation system utilizes EPR (Ethylene Propylene Rubber) compound type 3GI3, which provides superior electrical properties and resistance to thermal degradation compared to PVC or standard XLPE compounds. This EPR insulation is critical for withstanding the voltage stresses imposed by VFD operation.
For cables rated 6 kV and above, the construction includes both inner and outer semiconductive layers of semiconductive rubber. These field control layers ensure uniform electrical field distribution around the conductor, preventing localized stress concentrations that could lead to insulation breakdown. The outer semiconductive layer serves an additional critical function in VFD applications by providing a defined path for capacitive currents.
Multi-Layer Screening System
The screening architecture of (N)3GHSSYCY cables provides comprehensive electromagnetic interference (EMI) protection essential for VFD applications. The system includes a spiral arrangement of copper wires over the outer semiconductive layer of the cores, creating the primary earth conductor. A PVC inner sheath (type YM5 compound) provides mechanical separation and additional insulation. A monitoring conductor consisting of conductive tape serving and overall concentric copper wire spinning enables detection of outer damage during operation. An intermediate PVC sheath (type YM5) provides additional mechanical protection. Finally, an armor layer of braided galvanized steel wires offers exceptional mechanical protection and serves as an additional screening layer.
| Cable Component 电缆组件 | Material/Specification 材料/规格 | Function 功能 |
|---|---|---|
| Conductor 导体 | Stranded copper, Class 5 (DIN VDE 0295) 绞合铜,5类 | Current conduction, high flexibility 电流传导,高柔韧性 |
| Primary Insulation 主绝缘 | EPR Type 3GI3 EPR 3GI3型 | Electrical insulation, thermal stability 电气绝缘,热稳定性 |
| Field Control Layers 场控制层 | Semiconductive rubber 半导电橡胶 | Uniform electrical field distribution 均匀电场分布 |
| Earth Conductor 接地导体 | Spiral copper wires 螺旋铜线 | Primary grounding path 主接地路径 |
| Inner Sheath 内护套 | PVC Type YM5 PVC YM5型 | Mechanical separation, moisture barrier 机械分离,防潮屏障 |
| Monitoring System 监控系统 | Conductive tape + Cu wire 导电带 + 铜线 | Damage detection during operation 运行期间的损坏检测 |
| Armor 铠装 | Galvanized steel wire braid 镀锌钢丝编织 | Mechanical protection, EMI shielding 机械保护,EMI屏蔽 |
| Outer Sheath 外护套 | PVC Type YM5 PVC YM5型 | Environmental protection 环境保护 |
Source: Caledonian Cables – “N3GHSSYCY Medium-Voltage Cable” https://www.caledonian-cables.net/product/Mining_Cables/VDE/N3GHSSYCY.html
Additional Reference: Feichun Special Cable – “What is Mining, Drilling & Tunnelling Cable?” https://feichuncables.com/blog/what-is-mining-drilling-tunnelling-cable-solutions-for-surface-sub-surface-underground-operations/
Applications and Performance Advantages
应用和性能优势
The (N)3GHSSYCY cable construction makes it ideally suited for connection of mobile operating equipment in mines and underground excavations with hazardous environments. In stationary applications such as high-voltage transformers in mining and tunneling operations, the cable provides reliable performance under conditions that would quickly destroy conventional cables. The robust construction enables use in scenarios where the cable must be laid in containers and unwound as excavation work progresses, a common requirement in tunnel boring and mining advancement operations.
VFD Application Benefits
For VFD-controlled motors, the comprehensive screening system of (N)3GHSSYCY cables addresses all major failure mechanisms. The multi-layer metallic screening provides a low-impedance path for high-frequency common-mode currents, preventing them from circulating through motor bearings. The spiral copper earth conductor and steel wire braid armor combine to create symmetrical grounding that minimizes voltage differences between the drive enclosure and motor frame. The EPR insulation with semiconductive layers handles voltage spikes that exceed 1,500V without breakdown, protecting against insulation failure. The monitoring conductor system enables early detection of cable damage before it leads to catastrophic motor failure.
| Application Scenario 应用场景 | Environmental Challenges 环境挑战 | Cable Protection Features 电缆保护特性 |
|---|---|---|
| Underground Mining VFD Conveyors 地下采矿VFD输送机 | Mechanical stress, dust, moisture, explosive atmospheres 机械应力,粉尘,潮湿,爆炸性气体 | Steel wire armor, EPR insulation, comprehensive screening 钢丝铠装,EPR绝缘,全面屏蔽 |
| Tunnel Boring Machines (TBM) 隧道掘进机 | Continuous flexing, high vibration, VFD motor control 连续弯曲,高振动,VFD电机控制 | Class 5 flexible conductor, multi-layer protection, monitoring system 5级柔性导体,多层保护,监控系统 |
| Mobile Mining Equipment 移动采矿设备 | Frequent relocation, dragging, crush hazards 频繁移动,拖曳,挤压危险 | Galvanized steel braid, dual PVC sheaths, damage monitoring 镀锌钢编织,双PVC护套,损坏监控 |
| High-Voltage Transformers 高压变压器 | Voltage transients, electromagnetic interference 电压瞬变,电磁干扰 | Semiconductive field control, symmetrical grounding, high corona resistance 半导电场控制,对称接地,高电晕抗性 |
Compliance with Mining Safety Standards
Beyond VFD-specific requirements, (N)3GHSSYCY cables meet stringent mining safety regulations. The construction complies with VDE 0250 Part 605 specifications, which are recognized internationally for mining cable applications. The flame-retardant properties of the EPR insulation and PVC sheath compounds meet requirements for hazardous underground environments. The monitoring conductor system provides compliance with regulations requiring damage detection in safety-critical mining applications.
Source: Hybird Resources – “N3GHSSYCY Screened/PVC MV Mining Cable” https://hybirdresources.com/product/n3ghssycy-screened-pvc-mv-mining-cable
Installation Best Practices for VFD Applications
VFD应用的安装最佳实践
Proper installation of screened cables is equally critical as selecting the correct cable specification. Even the best-designed cable will fail to provide adequate protection if installation practices create paths for common-mode currents or compromise the screening effectiveness. Several key principles govern successful VFD cable installation in industrial environments.
Grounding and Bonding Requirements
The cable shield must be connected at both the drive end and motor end using electromagnetic compatibility (EMC) cable glands that provide 360-degree contact between the shield and the grounded enclosure. This creates the essential low-impedance return path for high-frequency currents. Standard cable glands that only contact the shield at discrete points are inadequate for VFD applications. The drive enclosure and motor frame must both be solidly connected to the same ground potential to minimize ground loops.
For maximum effectiveness, separate conduits should be used for input power cables and motor cables. When cables must cross, they should do so at 90-degree angles to minimize inductive coupling. Control and sensor cables should maintain physical separation from motor power cables, with crossings again at perpendicular angles when unavoidable.
Cable Length Considerations
Cable length significantly impacts the severity of VFD-related problems. On longer cable runs (typically over 30-50 meters for 480V systems), PWM pulses build upon each other, creating peak voltages that can quickly exceed the cable and motor insulation ratings. When cable length exceeds manufacturer recommendations, additional protection such as dv/dt filters at the drive output or termination networks at the motor may be necessary. The recommended maximum cable length varies with motor voltage, drive switching frequency, and cable capacitance, requiring careful system design for long-distance applications.
| Installation Practice 安装实践 | Correct Method 正确方法 | Common Error 常见错误 |
|---|---|---|
| Shield Termination 屏蔽端接 | 360° EMC gland at both ends 两端360°EMC接头 | Point contact or single-end grounding 点接触或单端接地 |
| Ground Continuity 接地连续性 | Drive and motor at same potential 驱动器和电机处于相同电位 | Separate ground points creating loops 独立接地点形成回路 |
| Cable Routing 电缆布线 | Separate conduit from input power 与输入电源分离的导管 | Bundling with input or control cables 与输入或控制电缆捆绑 |
| Cable Length 电缆长度 | As short as practical, observe maximums 尽可能短,遵守最大值 | Exceeding rated length without filters 超过额定长度而不使用滤波器 |
| Bending Radius 弯曲半径 | Follow VDE 0298-4 specifications 遵循VDE 0298-4规范 | Sharp bends damaging conductors 尖锐弯曲损坏导体 |
Source: Ecogate – “Should Shaft Grounding be Used When a Motor is Used with a Variable Frequency Drive?” https://www.ecogate.com/post/should-we-use-shaft-grounding-when-a-motor-is-used-with-a-variable-frequency-drive
Conclusion and Recommendations
结论和建议
The widespread adoption of variable frequency drives for motor control has created significant operational challenges that many industrial facilities have underestimated or entirely overlooked. While VFDs deliver undeniable benefits in energy efficiency and process control, their electrical characteristics fundamentally differ from traditional power sources in ways that can destroy motor bearings and insulation within weeks or months of operation. The financial impact of premature motor failures extends far beyond replacement costs, encompassing expensive unplanned downtime, lost production, and potential safety hazards.
Proper cable selection represents a critical but often neglected aspect of VFD system design. Standard power cables designed for sinusoidal AC operation lack the specialized insulation thickness, screening architecture, and grounding systems necessary to handle the high-frequency electrical disturbances created by pulse width modulation. The (N)3GHSSYCY screened mining cable construction, engineered to VDE 0250 Part 605 specifications, provides comprehensive protection against all major VFD-induced failure mechanisms through its combination of EPR insulation, multi-layer screening, symmetrical grounding, and robust mechanical protection.
For facilities operating VFD-controlled motors in demanding industrial environments, particularly mining and tunneling applications, investment in properly specified screened cables delivers substantial long-term value. The incremental cost difference between standard cables and properly screened VFD cables becomes negligible when compared against the costs of premature motor failures, emergency repairs, and operational disruptions. When combined with proper installation practices including 360-degree shield grounding, appropriate cable routing, and attention to cable length limitations, screened cables such as (N)3GHSSYCY provide reliable protection that enables VFD systems to deliver their intended benefits without compromising motor reliability.
Technical Recommendation Summary
For all new VFD installations and when replacing failed motors or cables in existing VFD systems, facilities should specify cables meeting or exceeding VDE 0250 Part 605 requirements with comprehensive screening, XLPE or EPR insulation rated for voltages above 1,200V, symmetrical or full-size ground conductors, and armor protection appropriate for the mechanical environment. Installation must employ EMC cable glands providing 360-degree shield contact at both drive and motor ends, with verification of proper grounding continuity throughout the system.
Contact Anhui Feichun Special Cable Co., Ltd.
联系安徽飞纯特种电缆有限公司
For technical specifications, quotations, or consultation regarding (N)3GHSSYCY screened mining cables and other specialized VFD cable solutions, contact our engineering team:


