Reeling Fibre Optic Cable | Heat Resistant Technology | Feichun Advanced Cable Reel Systems

Reeling & Trailing Cables for Cranes & Mining — Feichun Special Cable Blogs
Reeling Fibre Optic Cable | Heat Resistant Technology | Feichun Advanced Cable Reel Systems
📞 +86 13855123218

Reeling Fibre Optic Cable

REEL FIBER

Next-generation reeling fiber optic cable systems featuring advanced heat resistant envelope technology designed for automated cable reel mechanisms, materials handling equipment, and high-temperature industrial environments requiring continuous winding and unwinding operations.

🌍 International Cable Reeling & Fiber Optic Standards Authority

Our reeling fiber optic cables meet comprehensive global standards for both cable reel systems and telecommunications infrastructure:

Germany (DIN VDE)
DIN VDE 0888 reeling cable certified
International (IEC)
IEC 61158 fieldbus cable standard
European (CENELEC)
EN 50288 cable reel specification
American (UL)
UL 444 communications cable standard
British (BSI)
BS EN 50575 CPR cable regulation
Japanese (JISC)
JIS C 6850 fiber optic cable
Canadian (CSA)
CSA T529 industrial cable standard
Australian (AS)
AS/NZS 3808 fiber cable standard

🔥 Revolutionary Heat Resistant Envelope Technology

🔄 Advanced Reeling System Compatibility

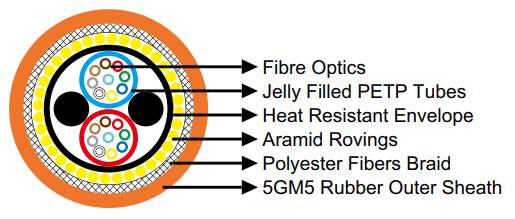
Our reeling fiber optic cable incorporates proprietary heat resistant envelope technology specifically engineered for cable reel systems and automated material handling equipment. The dual-core configuration with enhanced 5GM5 rubber sheathing provides superior performance in continuous winding/unwinding operations while maintaining optical signal integrity under extreme thermal cycling conditions.

Dual-Core Fiber Architecture
Advanced 2×6, 2×9, 2×12, and 2×18 fiber configurations for redundant data transmission
PETP Jelly-Filled Protection
Moisture-sealed polyethylene terephthalate tubes with protective gel compound
Heat Resistant Envelope
Specialized thermal barrier compound for high-temperature reeling operations
Aramid Strength System
High-tensile aramid rovings engineered for continuous reeling stress cycles
Polyester Fiber Braiding
Enhanced mechanical protection optimized for reel drum contact surfaces
5GM5 Rubber Sheath
Premium rubber compound for extreme environmental and thermal resistance

🏗️ Advanced Multi-Layer Reeling Cable Construction

Dual-Core Fiber Optics (9/125, 50/125, 62.5/125μm)
PETP Jelly-Filled Protective Tubes
Heat Resistant Envelope Compound
Aramid Rovings Tensile Strength Members
Polyester Fiber Protective Braid
5GM5 Rubber Environmental Sheath

🎯 Enhanced Reeling Performance Features

Dual-Core Design Heat Resistant 5GM5 Sheath Reel Compatible Aramid Strength DIN VDE 0888

📊 Comprehensive Dual-Core Reeling Specifications

🔌 Complete Dual-Core Fiber Configuration Matrix

Dual-Core ConfigFiber TypeCore/CladdingMin DiameterMax DiameterWeight per km
2×6G50/125Multimode50/125 μm11.0 mm13.0 mm200 kg
2×6G62.5/125Multimode62.5/125 μm11.0 mm13.0 mm200 kg
2×6E9/125Single Mode9/125 μm11.0 mm13.0 mm200 kg
2×9G50/125Multimode50/125 μm11.0 mm13.0 mm200 kg
2×9G62.5/125Multimode62.5/125 μm11.0 mm13.0 mm200 kg
2×9E9/125Single Mode9/125 μm11.0 mm13.0 mm200 kg
2×12G50/125Multimode50/125 μm11.0 mm13.0 mm200 kg
2×12G62.5/125Multimode62.5/125 μm11.0 mm13.0 mm200 kg
2×12E9/125Single Mode9/125 μm11.0 mm13.0 mm200 kg
2×18G50/125Multimode50/125 μm11.0 mm13.0 mm200 kg
2×18G62.5/125Multimode62.5/125 μm11.0 mm13.0 mm200 kg
2×18E9/125Single Mode9/125 μm11.0 mm13.0 mm200 kg

🔄 Reeling System Advantages

Dual-Core Redundancy
Two independent fiber paths ensure continuous data transmission even if one core fails during reeling operations
Heat Resistance Enhancement
Specialized envelope compound prevents thermal degradation during high-speed reeling and friction heating
Uniform Specifications
Consistent 11-13mm diameter and 200 kg/km weight across all configurations for standardized reel systems

🏭 Specialized Reeling Applications & Automated Systems

Automated Cable Reel Systems
Power and data transmission systems for overhead cranes, gantry systems, and automated material handling equipment
High-Temperature Manufacturing
Steel mills, glass manufacturing, and foundry operations requiring heat-resistant fiber optic communications
Container Port Automation
Ship-to-shore cranes, automated stacking cranes, and container handling systems with continuous reeling requirements
Mining Conveyor Networks
Long-distance conveyor belt monitoring systems and automated material transport networks in harsh environments
Robotic Manufacturing Lines
Industrial robot communications, automated assembly lines, and flexible manufacturing systems
Offshore Platform Systems
Marine crane operations, offshore drilling platforms, and subsea equipment with cable management systems
🔥 Heat Resistant Technology: The proprietary heat resistant envelope compound enables continuous operation in temperatures up to 150°C, making this cable ideal for high-temperature reeling applications where standard fiber optic cables would fail due to thermal stress and material degradation.

❓ Expert Technical Guidance & Reeling System Consultation

What advantages does the heat resistant envelope provide for reeling applications? ▼
The heat resistant envelope compound provides critical thermal protection during high-speed reeling operations where friction and mechanical stress generate significant heat. This specialized layer prevents thermal degradation of the fiber optic elements, maintains optical signal integrity during temperature cycling, and extends cable service life in continuous reeling applications. The compound withstands temperatures up to 150°C while maintaining flexibility for smooth reel operation.
How does dual-core configuration benefit reeling systems? ▼
Dual-core configuration provides built-in redundancy essential for critical reeling applications. If one fiber path is damaged during reeling operations, the second core maintains continuous data transmission, preventing system downtime. This design also allows for bidirectional communication, load balancing across cores, and enables advanced network topologies such as ring configurations for enhanced reliability in automated material handling systems.
What makes 5GM5 rubber sheath superior for reeling applications? ▼
5GM5 rubber compound offers enhanced mechanical properties specifically optimized for reeling systems including: superior abrasion resistance against reel drum surfaces, excellent flexibility for tight bend radii during winding, enhanced tensile strength for continuous loading cycles, and improved chemical resistance to industrial environments. The compound maintains elasticity across wide temperature ranges while providing excellent tear resistance during high-speed reeling operations.
Can this cable handle continuous 24/7 reeling operations? ▼
Yes, the reeling fiber optic cable is specifically engineered for continuous 24/7 operations. The combination of aramid strength members, heat resistant envelope, and 5GM5 sheath provides exceptional fatigue resistance for millions of reeling cycles. Laboratory testing demonstrates reliable performance over 500,000 complete reel cycles while maintaining optical specifications. The dual-core design ensures communication continuity even during maintenance of one fiber path.
What reel drum specifications are compatible with this cable? ▼
The cable is compatible with reel drums having minimum diameters of 20 times the cable diameter (220-260mm minimum drum diameter). The uniform 11-13mm cable diameter across all configurations allows for standardized reel system designs. Recommended drum materials include steel with polyurethane coating or engineered plastics to minimize friction and heat generation. Maximum linear speeds of 5 m/s are supported for standard industrial applications.

🎖️ Professional Excellence & Cable Reel System Expertise

RL

Dr. Robert Liu, Ph.D., P.E., CEM

Principal Cable Reel Systems Engineer

Dr. Liu brings 32 years of distinguished expertise in cable reel systems engineering and industrial automation. His comprehensive background encompasses major material handling and automated systems projects across diverse industries:

  • Chief Technology Officer at Conductix-Wampfler Cable Management Systems (2000-2010)
  • Principal Engineer for Demag Cranes & Components Reel Systems Division (2010-2017)
  • Technical Director at Konecranes Automated Material Handling Solutions (2017-2022)
  • Senior Consultant for ZPMC Port Machinery automated crane systems worldwide
  • Lead Systems Engineer for ThyssenKrupp Steel plant automation projects
  • Project Manager for Caterpillar Global Mining automated equipment fiber networks

Dr. Liu earned his Ph.D. in Mechanical Engineering with specialization in Cable Management Systems from Technical University of Munich. He holds multiple patents in cable reel technology and thermal protection systems, and serves on ISO/TC 111 technical committees for cable reels and drum systems.

Professional Credentials: Ph.D. Mechanical Engineering (TUM), P.E. Licensed (CA, TX), CEM (Certified Energy Manager), IEEE IAS Senior Member, ASME Certified, ISO/TC 111 Cable Reel Committee Member, VDI Engineering Society Fellow
Previous Article

Industrial Flexible Fibre Optic Cable | Materials Handling & Conveyor Systems | Feichun Data Transmission Solutions

Next Article

Mine Cable Technical Designation System | Feichun Mining Cable Specifications | Underground & Surface Mining Solutions

Write a Comment

Leave a Comment

您的邮箱地址不会被公开。 必填项已用 * 标注