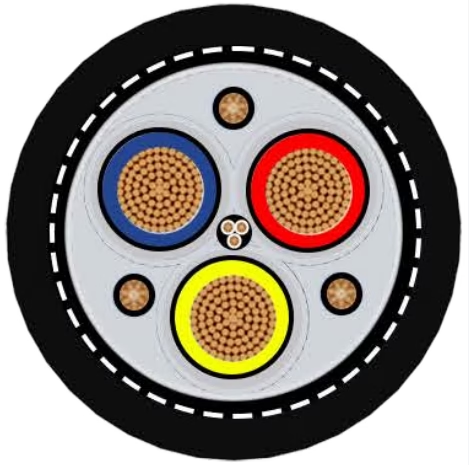
shovel cable

Hybrid Cable Innovation: Dual-Voltage Architecture for Building Lifts The FLEXIDRUM® BASKET LIFT 731 represents a revolutionary engineering approach to hoisting cables for building construction lifts. Unlike traditional single-voltage cables that require separate control and power conductors, the 731 integrates dual-voltage capability (300/500V control + 0.6/1kV power) into a single hybrid structure. This hybrid design is specifically engineered for modern building hoist systems operating in construction environments, where: Control circuits (300/500V) manage speed control, safety interlocks, load monitoring, and emergency descent systems Power circuits (0.6/1kV) drive the main hoist motor (typically 15–50 kW capacity) Single cable run simplifies installation—no separate routing for control vs. power, reducing labor costs ~30% Space efficiency eliminates need for dual-cable management on building facades Safety redundancy through separate insulation layers ensures control circuit failure doesn't disable power monitoring The BASKET LIFT 731's architecture is distinctly different from port crane cables (SPREADER 740/750) and terrestrial industrial cables, reflecting the unique requirements of vertical construction lift systems where personnel safety depends on reliable signal transmission alongside high-power motor control.

O que é o TENAX-SAS (N)TSCGEWOEU 3,6/6 kV: uma análise técnica aprofundada do cabo de média tensão de alta flexibilidade, alta resistência à tração e elevada resistência à abrasão para equipamentos móveis pesados de mineração

O TENAX-SAS (N)TSCGEWOEU 3,6/6 kV é um cabo de média tensão concebido para trailing e reeling em condições mecânicas severas, como pás elétricas, shovels, draglines e outros equipamentos móveis de grande porte em mineração. Seu valor técnico não está apenas na classe de tensão, mas no equilíbrio entre flexibilidade extrema em baixas temperaturas, robustez de bainha, resistência à tração contínua, integridade elétrica do sistema semicondutivo e estabilidade estrutural sob abrasão, torção, flexão repetitiva e deslocamentos contínuos sobre terreno agressivo.
The fundamental difference between mold-cured and continuous vulcanization processes lies in the physical pressure and thermal constraints applied to the rubber jacket during the cross-linking (vulcanization) phase. In continuous vulcanization, the extruded cable jacket enters a pressurized tube where steam or nitrogen provides only ambient fluid pressure (typically 20 to 100 psi), allowing microscopic air voids to persist within the rubber matrix—a manufacturing-efficient but mechanically compromising approach. In contrast, Nexans AmerCable's proprietary lead-mold curing process encloses the entire extruded cable within a continuous solid lead sheath that subjects the expanding rubber to extreme physical confinement pressure (1,000 to 3,000 psi or higher), forcing virtually all microscopic air voids out of the rubber and enabling optimal cross-linking of polymer chains. The resulting mold-cured jacket exhibits tensile strength 15 to 25 percent higher, tear resistance 20 to 40 percent superior, and abrasion resistance 25 to 50 percent greater than equivalent continuous vulcanization designs—advantages that justify the Tiger Brand's premium positioning and explain its dominant market share in high-altitude Chilean and Peruvian copper mining where cables endure continuous abrasion on jagged rocks, mechanical crushing from heavy loads, and environmental stress from sulfide ore compounds.

Mold-Cured Jacket: AmerCable Tiger Brand vs. Continuous Vulcanization – Why Is Mold-Cured Considered Tougher?

The fundamental difference between mold-cured and continuous vulcanization processes lies in the physical pressure and thermal constraints applied to the rubber jacket during the cross-linking (vulcanization) phase. In continuous vulcanization, the extruded cable jacket enters a pressurized tube where steam or nitrogen provides only ambient fluid pressure (typically 20 to 100 psi), allowing microscopic air voids to persist within the rubber matrix—a manufacturing-efficient but mechanically compromising approach. In contrast, Nexans AmerCable’s proprietary lead-mold curing process encloses the entire extruded cable within a continuous solid lead sheath that subjects the expanding rubber to extreme physical confinement pressure (1,000 to 3,000 psi or higher), forcing virtually all microscopic air voids out of the rubber and enabling optimal cross-linking of polymer chains. The resulting mold-cured jacket exhibits tensile strength 15 to 25 percent higher, tear resistance 20 to 40 percent superior, and abrasion resistance 25 to 50 percent greater than equivalent continuous vulcanization designs—advantages that justify the Tiger Brand’s premium positioning and explain its dominant market share in high-altitude Chilean and Peruvian copper mining where cables endure continuous abrasion on jagged rocks, mechanical crushing from heavy loads, and environmental stress from sulfide ore compounds.
Type SHD-GC 3/C 4/0 AWG 8kV trailing cable, rated for 321 to 327 amperes continuous current at sea level (0 meters) assuming typical mining conditions with natural air cooling, experiences substantial reduction in current-carrying capacity when deployed at 4,000 meters elevation in the Andes Mountains. At 4,000 meters, the atmospheric pressure is only approximately 60 percent of sea-level pressure, and air density is reduced proportionally. This thin-air environment reduces the cable's cooling efficiency dramatically, resulting in derated ampacity of approximately 185 to 210 amperes—a reduction of 40 to 45 percent compared to sea-level capacity. This derating is not optional or conservative—it is physically necessary to prevent the cable conductor from exceeding the maximum allowable operating temperature of 90°C under continuous load. If a cable rated at 321A at sea level were operated at full sea-level ampacity while installed at 4,000 meters elevation, the conductor temperature would rise to approximately 120°C to 140°C or higher, severely accelerating insulation degradation and risking catastrophic failure within months. The derating magnitude is driven by fundamental thermodynamic principles: as altitude increases and air density decreases, the convective heat transfer coefficient that governs how efficiently the cable surface transfers heat to the surrounding air decreases proportionally. The relationship between air density and cooling efficiency is not linear—it follows approximately the 0.6 power relationship, meaning that reducing air density to 60 percent of sea-level value reduces cooling efficiency to approximately 70 percent. Additionally, in high-altitude Andes mining regions where ambient temperatures reach 25°C to 35°C in tropical regions or 40°C to 50°C in equipment enclosures, the combined effect of altitude derating plus temperature derating can reduce ampacity to values as low as 150 to 160 amperes—less than half the sea-level rating. Understanding and properly accounting for altitude derating in equipment selection, protection device settings, and operational procedures is essential for safe and reliable operation of power distribution systems at high-altitude mining facilities.

High-Altitude Ampacity Derating: How Does Operating at 4,000m in the Andes Mountains Affect Type SHD-GC 3/C 4/0 AWG 8kV Cable Current Capacity?

Type SHD-GC 3/C 4/0 AWG 8kV trailing cable, rated for 321 to 327 amperes continuous current at sea level (0 meters) assuming typical mining conditions with natural air cooling, experiences substantial reduction in current-carrying capacity when deployed at 4,000 meters elevation in the Andes Mountains. At 4,000 meters, the atmospheric pressure is only approximately 60 percent of sea-level pressure, and air density is reduced proportionally. This thin-air environment reduces the cable’s cooling efficiency dramatically, resulting in derated ampacity of approximately 185 to 210 amperes—a reduction of 40 to 45 percent compared to sea-level capacity. This derating is not optional or conservative—it is physically necessary to prevent the cable conductor from exceeding the maximum allowable operating temperature of 90°C under continuous load. If a cable rated at 321A at sea level were operated at full sea-level ampacity while installed at 4,000 meters elevation, the conductor temperature would rise to approximately 120°C to 140°C or higher, severely accelerating insulation degradation and risking catastrophic failure within months. The derating magnitude is driven by fundamental thermodynamic principles: as altitude increases and air density decreases, the convective heat transfer coefficient that governs how efficiently the cable surface transfers heat to the surrounding air decreases proportionally. The relationship between air density and cooling efficiency is not linear—it follows approximately the 0.6 power relationship, meaning that reducing air density to 60 percent of sea-level value reduces cooling efficiency to approximately 70 percent. Additionally, in high-altitude Andes mining regions where ambient temperatures reach 25°C to 35°C in tropical regions or 40°C to 50°C in equipment enclosures, the combined effect of altitude derating plus temperature derating can reduce ampacity to values as low as 150 to 160 amperes—less than half the sea-level rating. Understanding and properly accounting for altitude derating in equipment selection, protection device settings, and operational procedures is essential for safe and reliable operation of power distribution systems at high-altitude mining facilities.
The standard (N)TSCGEWÖU 3x50+3x25/3 trailing cable is technically rated for ambient temperatures down to approximately -10°C to -15°C under normal industrial conditions according to DIN VDE 0250 Part 813, with the 5GM5 CPE (chlorinated polyethylene) rubber jacket remaining flexible and maintaining mechanical integrity within this range. However, operating this cable in Arctic mining environments at sustained -40°C temperatures requires significant engineering reevaluation and is not recommended without specialized modifications and enhanced installation protocols. While the cable does not spontaneously fail at -40°C, the rubber jacket becomes progressively more rigid and brittle, and the minimum allowable bending radius must be expanded from the standard 15D (15 times the outer diameter) to approximately 25D to 30D or greater to prevent jacket cracking during dynamic reeling operations. At -50°C, which occurs frequently in Siberia and parts of Northern Canada during winter, standard TECWATER-family cables experience material brittleness that pushes them toward structural failure risk even without bending stress. A cable suitable for -15°C temperate mining operations is fundamentally different in its application safety profile from a cable operating continuously at -40°C in an open-pit mine where the cable must flex regularly during equipment deployment and retrieval. The distinction between "technically possible" and "operationally safe" is critical to understand: equipment that operates at extreme cold requires more than just survival—it requires predictable, controlled behavior under stress. The standard (N)TSCGEWÖU can survive brief exposure to -40°C without immediate failure, but extended service in this temperature regime demands either specification of cold-hardened alternatives or acceptance of significant operational constraints.

Arctic Mining Cable Performance: Is (N)TSCGEWÖU 3×50+3×25/3 Rated for -40°C Extreme Cold Conditions in Russia and Canada?

The standard (N)TSCGEWÖU 3×50+3×25/3 trailing cable is technically rated for ambient temperatures down to approximately -10°C to -15°C under normal industrial conditions according to DIN VDE 0250 Part 813, with the 5GM5 CPE (chlorinated polyethylene) rubber jacket remaining flexible and maintaining mechanical integrity within this range. However, operating this cable in Arctic mining environments at sustained -40°C temperatures requires significant engineering reevaluation and is not recommended without specialized modifications and enhanced installation protocols. While the cable does not spontaneously fail at -40°C, the rubber jacket becomes progressively more rigid and brittle, and the minimum allowable bending radius must be expanded from the standard 15D (15 times the outer diameter) to approximately 25D to 30D or greater to prevent jacket cracking during dynamic reeling operations. At -50°C, which occurs frequently in Siberia and parts of Northern Canada during winter, standard TECWATER-family cables experience material brittleness that pushes them toward structural failure risk even without bending stress. A cable suitable for -15°C temperate mining operations is fundamentally different in its application safety profile from a cable operating continuously at -40°C in an open-pit mine where the cable must flex regularly during equipment deployment and retrieval. The distinction between “technically possible” and “operationally safe” is critical to understand: equipment that operates at extreme cold requires more than just survival—it requires predictable, controlled behavior under stress. The standard (N)TSCGEWÖU can survive brief exposure to -40°C without immediate failure, but extended service in this temperature regime demands either specification of cold-hardened alternatives or acceptance of significant operational constraints.
Type SHD-GC 3/C #1 AWG 8kV trailing cable has a DC resistance of approximately 0.161 ohms per kilometer measured at the reference temperature of 20°C (68°F). This DC resistance value represents the pure ohmic resistance of the copper conductor when direct current flows through it—a condition that occurs in short-circuit analysis and DC testing procedures. However, when this same cable carries the alternating current typical of mining equipment operations (at the standard operating temperature of 90°C), the AC resistance increases to approximately 0.363 ohms per kilometer due to the combined effects of temperature rise and skin effect phenomena. The substantial difference between 0.161 Ω/km (DC, 20°C) and 0.363 Ω/km (AC, 90°C)—more than a 2.25 times increase—demonstrates a critical principle that engineers must account for in real-world voltage drop calculations: laboratory DC resistance values are not directly applicable to field voltage drop analysis. The cable features three 107.2 mm² (1 AWG equivalent) phase conductors of Class 5 tinned copper, with an additional ground-check conductor for continuous monitoring of cable integrity during operation, an outer diameter of approximately 53–58 mm, and a total weight of approximately 6,200–6,800 kg/km. Understanding both the DC baseline resistance and the elevated AC resistance at operating temperature is essential for accurately predicting voltage drop over long cable runs in open-pit mining operations where power distribution distances frequently exceed 500 meters.

Voltage Drop Calculation: Resistance (Ohms/km) for Type SHD-GC 3/C #1 AWG 8kV Trailing Cable

Type SHD-GC 3/C #1 AWG 8kV trailing cable has a DC resistance of approximately 0.161 ohms per kilometer measured at the reference temperature of 20°C (68°F). This DC resistance value represents the pure ohmic resistance of the copper conductor when direct current flows through it—a condition that occurs in short-circuit analysis and DC testing procedures. However, when this same cable carries the alternating current typical of mining equipment operations (at the standard operating temperature of 90°C), the AC resistance increases to approximately 0.363 ohms per kilometer due to the combined effects of temperature rise and skin effect phenomena. The substantial difference between 0.161 Ω/km (DC, 20°C) and 0.363 Ω/km (AC, 90°C)—more than a 2.25 times increase—demonstrates a critical principle that engineers must account for in real-world voltage drop calculations: laboratory DC resistance values are not directly applicable to field voltage drop analysis. The cable features three 107.2 mm² (1 AWG equivalent) phase conductors of Class 5 tinned copper, with an additional ground-check conductor for continuous monitoring of cable integrity during operation, an outer diameter of approximately 53–58 mm, and a total weight of approximately 6,200–6,800 kg/km. Understanding both the DC baseline resistance and the elevated AC resistance at operating temperature is essential for accurately predicting voltage drop over long cable runs in open-pit mining operations where power distribution distances frequently exceed 500 meters.
The continuous ampacity of (N)TSCGEWÖU 3x120+3x70/3 12/20kV flexible reeling cable is 360 amperes when operating as a single conductor run in free air at the reference condition of 30°C ambient temperature and 90°C conductor operating temperature according to VDE 0250-813 and DIN VDE 0298-4 standards. For tunnel boring machine cutterhead power supply applications where the cable is installed in the constrained environment of a TBM backup gantry system—bundled alongside control cables, communication lines, and other power feeders—and subjected to frequent mechanical stress from dragging and reeling operations, the practical safe ampacity derates to approximately 260–285 amperes depending on specific installation geometry, tunnel temperature profile, and frequency of mechanical cycling. These two ampacity values represent the boundary between theoretical maximum current capacity and the practical operating limit for reliable power delivery to a 2–3 megawatt main cutterhead drive motor in a hard-rock tunneling or soft-ground excavation system. Understanding where these values come from and how they apply to specific TBM configurations is essential for preventing unexpected power loss to the cutterhead, which could force a full machine shutdown and result in schedule delays of weeks or months in confined underground construction.

TBM Cutterhead Power Supply: How to correctly size (N)TSCGEWÖU 3×120+3×70/3 12/20kV flexible reeling cable for tunnel boring machine main drive systems 

The continuous ampacity of (N)TSCGEWÖU 3×120+3×70/3 12/20kV flexible reeling cable is 360 amperes when operating as a single conductor run in free air at the reference condition of 30°C ambient temperature and 90°C conductor operating temperature according to VDE 0250-813 and DIN VDE 0298-4 standards. For tunnel boring machine cutterhead power supply applications where the cable is installed in the constrained environment of a TBM backup gantry system—bundled alongside control cables, communication lines, and other power feeders—and subjected to frequent mechanical stress from dragging and reeling operations, the practical safe ampacity derates to approximately 260–285 amperes depending on specific installation geometry, tunnel temperature profile, and frequency of mechanical cycling. These two ampacity values represent the boundary between theoretical maximum current capacity and the practical operating limit for reliable power delivery to a 2–3 megawatt main cutterhead drive motor in a hard-rock tunneling or soft-ground excavation system. Understanding where these values come from and how they apply to specific TBM configurations is essential for preventing unexpected power loss to the cutterhead, which could force a full machine shutdown and result in schedule delays of weeks or months in confined underground construction.
Type SHD-GC 3/C #1 AWG 8kV trailing cable is approximately 0.410 Ohms/km at 20°C reference temperature for a single conductor, calculated from the copper's material resistivity combined with the #1 AWG conductor cross-section (approximately 42.4 mm² or 53,486 circular mils). This resistance value increases to approximately 0.495 Ohms/km at 90°C operating temperature due to copper's positive temperature coefficient of resistance. For a complete three-phase circuit using this cable type, the total circuit resistance including all three phase conductors but excluding the ground return path is approximately 0.410 Ohms/km at 20°C or 0.495 Ohms/km at 90°C. When operating a mine shovel or dragline drawing 150–160 amperes over a typical 1,000-meter (1 km) cable run from the mine substation to the equipment, the three-phase voltage drop across this cable is approximately 55–70 volts at the reference condition, representing a drop of roughly 0.75–1.0% from the 8,000-volt nominal supply. This voltage drop magnitude is acceptable for most mining equipment applications and remains within typical power system design standards that permit up to 2–3% voltage drop on secondary feeder circuits. The physical mechanism behind this resistance is the collision of free electrons within the copper lattice structure, where random thermal motion of atoms creates an effective "friction" that opposes electron flow, converting electrical energy into heat at a rate proportional to I²R.

Voltage Drop Calculation: What is the DC resistance (Ohms/km) for Type SHD-GC 3/C #1 AWG 8kV trailing cable? 

Type SHD-GC 3/C #1 AWG 8kV trailing cable is approximately 0.410 Ohms/km at 20°C reference temperature for a single conductor, calculated from the copper’s material resistivity combined with the #1 AWG conductor cross-section (approximately 42.4 mm² or 53,486 circular mils). This resistance value increases to approximately 0.495 Ohms/km at 90°C operating temperature due to copper’s positive temperature coefficient of resistance. For a complete three-phase circuit using this cable type, the total circuit resistance including all three phase conductors but excluding the ground return path is approximately 0.410 Ohms/km at 20°C or 0.495 Ohms/km at 90°C. When operating a mine shovel or dragline drawing 150–160 amperes over a typical 1,000-meter (1 km) cable run from the mine substation to the equipment, the three-phase voltage drop across this cable is approximately 55–70 volts at the reference condition, representing a drop of roughly 0.75–1.0% from the 8,000-volt nominal supply. This voltage drop magnitude is acceptable for most mining equipment applications and remains within typical power system design standards that permit up to 2–3% voltage drop on secondary feeder circuits. The physical mechanism behind this resistance is the collision of free electrons within the copper lattice structure, where random thermal motion of atoms creates an effective “friction” that opposes electron flow, converting electrical energy into heat at a rate proportional to I²R.
The nominal outer diameter of a Type SHD-GC 3/C 350 MCM 15kV flexible mining trailing cable is approximately 73 mm (2.87 inches), with a maximum permissible outer diameter of approximately 74.9 mm (2.95 inches) per ICEA S-75-381 and NEMA WC-58 standards. The approximate weight of this specific cable geometry is 10,900 kg/km (7,300 lbs/1000 ft). It features three 350 MCM (177 mm² equivalent) main power conductors rated for 435 amperes continuous operation, supplemented by two 2/0 AWG earth conductors and one 6 AWG ground-check monitoring conductor for enhanced mining safety systems. The distinction between nominal (design target) and maximum (allowable limit) outer diameter is critical for mining operations because reel systems, conduit systems, and terminal connectors are engineered based on these dimensional constraints. A cable that exceeds the maximum outer diameter will not fit into equipment designed for the nominal specification, creating logistics delays and operational disruptions that cost far more than any cable savings.

What is the Maximum Outer Diameter of Type SHD-GC 3/C 350 MCM 15kV Mining Cable?

The nominal outer diameter of a Type SHD-GC 3/C 350 MCM 15kV flexible mining trailing cable is approximately 73 mm (2.87 inches), with a maximum permissible outer diameter of approximately 74.9 mm (2.95 inches) per ICEA S-75-381 and NEMA WC-58 standards. The approximate weight of this specific cable geometry is 10,900 kg/km (7,300 lbs/1000 ft). It features three 350 MCM (177 mm² equivalent) main power conductors rated for 435 amperes continuous operation, supplemented by two 2/0 AWG earth conductors and one 6 AWG ground-check monitoring conductor for enhanced mining safety systems. The distinction between nominal (design target) and maximum (allowable limit) outer diameter is critical for mining operations because reel systems, conduit systems, and terminal connectors are engineered based on these dimensional constraints. A cable that exceeds the maximum outer diameter will not fit into equipment designed for the nominal specification, creating logistics delays and operational disruptions that cost far more than any cable savings.
Ampacity is the maximum electric current that a conductor can safely carry continuously without exceeding a specified temperature limit, usually 90°C for power cables used in mining and industrial applications. The word itself is a contraction of "ampere" and "capacity," and it represents a fundamental constraint imposed by the physics of electrical resistance and heat dissipation. Understanding ampacity is not an academic exercise — it is the critical foundation for ensuring that your mining equipment receives reliable power, that cables do not overheat and fail prematurely, and that your operation avoids unplanned downtime due to cable damage or failure. 载流量是导体在不超过指定温度限值(通常为90°C)的条件下能连续安全承载的最大电流。

Ampacity Rating Guide: How Much Current Can a Type SHD-GC 3/C 4/0 AWG 8kV Cable Handle?

Ampacity is the maximum electric current that a conductor can safely carry continuously without exceeding a specified temperature limit, usually 90°C for power cables used in mining and industrial applications. The word itself is a contraction of “ampere” and “capacity,” and it represents a fundamental constraint imposed by the physics of electrical resistance and heat dissipation. Understanding ampacity is not an academic exercise — it is the critical foundation for ensuring that your mining equipment receives reliable power, that cables do not overheat and fail prematurely, and that your operation avoids unplanned downtime due to cable damage or failure. 载流量是导体在不超过指定温度限值(通常为90°C)的条件下能连续安全承载的最大电流。
When electrical engineers and equipment operators discuss the capacity of a dragline or shovel reeling cable, they often refer to a specification that seems disconnected from the typical electrical characteristics — the maximum permissible tensile load, expressed in units of pounds per thousand circular mills (lbs/mcm). This specification is fundamentally different from ampacity (which measures the cable's ability to safely carry electrical current) or voltage rating (which specifies the insulation quality). Instead, tensile load capacity describes the maximum mechanical force that the cable can withstand before the metallic conductors themselves begin to yield, stretch, or break. For a reeling cable used on heavy dragline or shovel equipment, this mechanical specification is often more critical to equipment safety and service life than the electrical specifications, because the cable is typically exposed to enormous pulling forces that can exceed the weight of the equipment being supported.

Type SHD-GC (Reeling): Maximum Permissible Tensile Load for Heavy-Duty Dragline Cable Reels

When electrical engineers and equipment operators discuss the capacity of a dragline or shovel reeling cable, they often refer to a specification that seems disconnected from the typical electrical characteristics — the maximum permissible tensile load, expressed in units of pounds per thousand circular mills (lbs/mcm). This specification is fundamentally different from ampacity (which measures the cable’s ability to safely carry electrical current) or voltage rating (which specifies the insulation quality). Instead, tensile load capacity describes the maximum mechanical force that the cable can withstand before the metallic conductors themselves begin to yield, stretch, or break. For a reeling cable used on heavy dragline or shovel equipment, this mechanical specification is often more critical to equipment safety and service life than the electrical specifications, because the cable is typically exposed to enormous pulling forces that can exceed the weight of the equipment being supported.
The selection of appropriate trailing cables for surface mining draglines represents a critical engineering decision that directly impacts operational efficiency, safety, and total cost of ownership. Dragline excavators, among the largest mobile land machines in operation, require specialized heavy-duty trailing cables capable of delivering high-voltage power (typically 2 kV to 35 kV) while withstanding extreme mechanical stresses including constant flexing, crushing forces, abrasion, and environmental exposure to ultraviolet radiation, temperature extremes, and moisture. This technical analysis examines the comparative merits of Nexans AmerCable's Tiger Brand premium mold-cured cables versus generic Type SHD-GC alternatives, focusing specifically on the critical importance of jacket construction technology in determining long-term performance and reliability in surface mining dragline applications.

Nexans AmerCable Tiger Brand vs. Type SHD-GC: Finding a Compatible Mold-Cured Jacket Cable for Surface Mining Draglines

The selection of appropriate trailing cables for surface mining draglines represents a critical engineering decision that directly impacts operational efficiency, safety, and total cost of ownership. Dragline excavators, among the largest mobile land machines in operation, require specialized heavy-duty trailing cables capable of delivering high-voltage power (typically 2 kV to 35 kV) while withstanding extreme mechanical stresses including constant flexing, crushing forces, abrasion, and environmental exposure to ultraviolet radiation, temperature extremes, and moisture. This technical analysis examines the comparative merits of Nexans AmerCable’s Tiger Brand premium mold-cured cables versus generic Type SHD-GC alternatives, focusing specifically on the critical importance of jacket construction technology in determining long-term performance and reliability in surface mining dragline applications.
Type 409 cables represent a specialized category of flexible mining cables designed specifically for demanding applications in material handling equipment, surface mining operations, and industrial environments. These cables are manufactured according to the Australian and New Zealand Standard AS/NZS 2802:2000, which establishes rigorous requirements for reeling and trailing cables used in mining and general industrial applications outside underground coal mining environments. (409型电缆是专为物料搬运设备、露天采矿作业和工业环境中的高要求应用而设计的一类特种柔性矿用电缆。这些电缆按照澳大利亚和新西兰标准AS/NZS 2802:2000制造,该标准对用于煤矿井下以外的采矿和一般工业应用的卷筒电缆和拖曳电缆制定了严格要求。)

TENAX-PUR (N)TSCGEH3S I 6 – 10 KV

TENAX-PUR is a premium medium voltage trailing cable engineered specifically for power supply to large mobile mining equipment such as shovels and draglines. The cable features an extremely robust polyurethane (PUR) outer sheath that delivers exceptional performance against abrasion and tearing, maintaining full flexibility even in extreme cold conditions down to -50°C. Available in orange, yellow, or custom colors to meet specific operational requirements. TENAX-PUR 是一种专为大型移动采矿设备(如电铲和拉斗铲)供电而设计的优质中压拖曳电缆。该电缆采用极其坚固的聚氨酯(PUR)外护套,在磨损和撕裂方面提供卓越的性能,即使在低至-50°C的极端寒冷条件下也能保持充分的柔韧性。可提供橙色、黄色或定制颜色以满足特定操作要求。
TSCGECEWÖU, NTSCGECEWÖU, TSKCGECWOEU, TSCGEWOEU, NSSHOEU, NTSCGEWOEU-CH, German mining cable, DIN cable, VDE cable, German cable standard, coal cutter cable CH, festoon cable FN, trailing cable W, screened cable designation, EPR mining cable

Joy Global (Komatsu) 7LS Longwall Shearer: (N)TSCGECEWÖU Drag Chain Cable Robustness Analysis

TSCGECEWÖU, NTSCGECEWÖU, TSKCGECWOEU, TSCGEWOEU, NSSHOEU, NTSCGEWOEU-CH, German mining cable, DIN cable, VDE cable, German cable standard, coal cutter cable CH, festoon cable FN, trailing cable W, screened cable designation, EPR mining cable
The maximum allowable pilot loop resistance for Type 450 mining cables operating with Ampcontrol earth continuity relays represents a critical electrical parameter that directly impacts mine safety and operational reliability. This comprehensive technical analysis examines the interaction between AS/NZS 2802:2000 Type 450 cable specifications and Ampcontrol relay requirements, providing mining engineers and electrical designers with authoritative guidance for proper system design and selection. 与Ampcontrol地电连续继电器配合使用的Type 450矿用电缆的最大允许导向回路电阻是一个直接影响矿山安全和运行可靠性的关键电气参数。本全面技术分析检查了AS/NZS 2802:2000 Type 450电缆规格与Ampcontrol继电器要求之间的相互作用,为矿业工程师和电气设计师提供了正确系统设计和选择的权威指导。

Pilot Core Resistance: What is the Maximum Allowable Pilot Loop Resistance (Ohms) for a Type 450 Cable to Function with Ampcontrol Relays?

The maximum allowable pilot loop resistance for Type 450 mining cables operating with Ampcontrol earth continuity relays represents a critical electrical parameter that directly impacts mine safety and operational reliability. This comprehensive technical analysis examines the interaction between AS/NZS 2802:2000 Type 450 cable specifications and Ampcontrol relay requirements, providing mining engineers and electrical designers with authoritative guidance for proper system design and selection. 与Ampcontrol地电连续继电器配合使用的Type 450矿用电缆的最大允许导向回路电阻是一个直接影响矿山安全和运行可靠性的关键电气参数。本全面技术分析检查了AS/NZS 2802:2000 Type 450电缆规格与Ampcontrol继电器要求之间的相互作用,为矿业工程师和电气设计师提供了正确系统设计和选择的权威指导。
Type 409 cables represent a specialized category of flexible mining cables designed specifically for demanding applications in material handling equipment, surface mining operations, and industrial environments. These cables are manufactured according to the Australian and New Zealand Standard AS/NZS 2802:2000, which establishes rigorous requirements for reeling and trailing cables used in mining and general industrial applications outside underground coal mining environments. (409型电缆是专为物料搬运设备、露天采矿作业和工业环境中的高要求应用而设计的一类特种柔性矿用电缆。这些电缆按照澳大利亚和新西兰标准AS/NZS 2802:2000制造,该标准对用于煤矿井下以外的采矿和一般工业应用的卷筒电缆和拖曳电缆制定了严格要求。)

Stacker Reclaimers: What is the Minimum Bending Radius for Type 409 Cables Used on High-Speed Stacker-Reclaimer Drums?

Type 409 cables represent a specialized category of flexible mining cables designed specifically for demanding applications in material handling equipment, surface mining operations, and industrial environments. These cables are manufactured according to the Australian and New Zealand Standard AS/NZS 2802:2000, which establishes rigorous requirements for reeling and trailing cables used in mining and general industrial applications outside underground coal mining environments. (409型电缆是专为物料搬运设备、露天采矿作业和工业环境中的高要求应用而设计的一类特种柔性矿用电缆。这些电缆按照澳大利亚和新西兰标准AS/NZS 2802:2000制造,该标准对用于煤矿井下以外的采矿和一般工业应用的卷筒电缆和拖曳电缆制定了严格要求。)
For a 500-meter length of Type 440 11kV mining cable, the required shipping drum dimensions are fundamentally determined by the cable's minimum bend radius and physical dimensions. Based on industry standards from AS/NZS 2802:2000 and IEC 60502-2, proper drum sizing ensures cable integrity during transportation and prevents damage to the cable's internal structure, particularly the semiconductive screens and EPR insulation critical for medium voltage applications. 对于500米长的Type 440 11kV矿用电缆,所需的运输卷筒尺寸主要由电缆的最小弯曲半径和物理尺寸决定。根据AS/NZS 2802:2000和IEC 60502-2的行业标准,正确的卷筒尺寸可确保运输过程中的电缆完整性,并防止损坏电缆的内部结构,特别是对中压应用至关重要的半导体屏蔽层和EPR绝缘层。

Drum Dimensions for Type 440 11kV Cable: Engineering Specification Guide

For a 500-meter length of Type 440 11kV mining cable, the required shipping drum dimensions are fundamentally determined by the cable’s minimum bend radius and physical dimensions. Based on industry standards from AS/NZS 2802:2000 and IEC 60502-2, proper drum sizing ensures cable integrity during transportation and prevents damage to the cable’s internal structure, particularly the semiconductive screens and EPR insulation critical for medium voltage applications. 对于500米长的Type 440 11kV矿用电缆,所需的运输卷筒尺寸主要由电缆的最小弯曲半径和物理尺寸决定。根据AS/NZS 2802:2000和IEC 60502-2的行业标准,正确的卷筒尺寸可确保运输过程中的电缆完整性,并防止损坏电缆的内部结构,特别是对中压应用至关重要的半导体屏蔽层和EPR绝缘层。
The proper application of tightening torque to phase connectors in high-voltage cable terminations is one of the most critical yet frequently overlooked aspects of electrical installation work. When terminating Type 450 cables at 33kV, the connector torque directly determines the quality and reliability of the electrical connection, affecting both the immediate performance and long-term service life of the installation. Understanding the correct torque specifications and their underlying principles is essential for ensuring safe, code-compliant, and maintenance-free operation in demanding mining and industrial environments. 在高压电缆终端中对相连接器施加正确的紧固扭矩是电气安装工作中最关键但经常被忽视的方面之一。在33kV终接Type 450电缆时,连接器扭矩直接决定电气连接的质量和可靠性。

Torque Settings: What is the Recommended Tightening Torque for Phase Connectors in a Type 450 33kV Termination?

The proper application of tightening torque to phase connectors in high-voltage cable terminations is one of the most critical yet frequently overlooked aspects of electrical installation work. When terminating Type 450 cables at 33kV, the connector torque directly determines the quality and reliability of the electrical connection, affecting both the immediate performance and long-term service life of the installation. Understanding the correct torque specifications and their underlying principles is essential for ensuring safe, code-compliant, and maintenance-free operation in demanding mining and industrial environments. 在高压电缆终端中对相连接器施加正确的紧固扭矩是电气安装工作中最关键但经常被忽视的方面之一。在33kV终接Type 450电缆时,连接器扭矩直接决定电气连接的质量和可靠性。
The short answer is yes, damaged Type 441 reeling cables can be spliced underground using resin joint kits that comply with AS/NZS 1747 standards, provided specific conditions are met and proper procedures are followed. However, understanding when, why, and how such repairs should be performed requires examining the cable construction, applicable standards, and field repair methodologies that govern mining cable maintenance practices across Australia, New Zealand, and similar international mining operations.

Can you splice a damaged Type 441 reeling cable underground using a Resin Joint Kit (AS/NZS 1747)?

The short answer is yes, damaged Type 441 reeling cables can be spliced underground using resin joint kits that comply with AS/NZS 1747 standards, provided specific conditions are met and proper procedures are followed. However, understanding when, why, and how such repairs should be performed requires examining the cable construction, applicable standards, and field repair methodologies that govern mining cable maintenance practices across Australia, New Zealand, and similar international mining operations.
Mining, drilling, and tunnelling cables represent a specialized category of electrical cables engineered to withstand the extreme conditions found in extractive industry operations. Unlike standard industrial cables, these cables must endure continuous mechanical stress from reeling and unreeling operations, exposure to ultraviolet radiation in surface mining, salt-water submersion in offshore drilling, contact with oils and greases from machinery, and the abrasive conditions of underground environments. The demanding nature of these applications requires cables with exceptional durability, flexibility, and resistance to environmental factors that would rapidly degrade conventional cables.

What is Mining, Drilling & Tunnelling Cable? Solutions for Surface, Sub-Surface & Underground Operations

(N)3GHSSHCH – 3.6/6kV, 6/10kV, 8.7/15kV, 12/20kV (N)3GHSSYCY – 3.6/6kV, 6/10kV, 8.7/15kV, 12/20kV (N)SSCHÖU-J – 0.6/1kV (N)SHÖU O/J – 0.6/1kV NSSHÖU O/J – 0.6/1kV NSSHÖU 3E – 0.6/1kV NSSHÖU 3E + ST – 0.6/1kV (N)TMCGEWÖU – 3.6/6kV to 18/30kV (N)TSCGEWÖU – 3.6/6kV to 18/30kV (N)TSCGEWÖU ZH – 3.6/6kV to 12/20kV (N)TSCGEWÖU ATB – 3.6/6kV to 12/20kV (N)TSCGEWÖU FO – 3.6/6kV to 12/20kV (N)TSCGEWÖU Submersible – 3.6/6kV to 12/20kV (N)TSKCGEWÖU – 3.6/6kV to 18/30kV (N)TSCGECEWÖU – 3.6/6kV to 12/20kV (N)TSCGECEWÖU ATB – 3.6/6kV to 12/20kV (N)TSCGECEWÖU ATB GCC – 1.8/3kV to 12/20kV (N)TSCGECEWÖU Submersible – 3.6/6kV to 12/20kV (N)TSCGECECWÖU – 3.6/6kV to 12/20kV (N)TSCGECECWÖU ZH – 3.6/6kV to 12/20kV R-(N)TSCGEWÖU + FO – 3.6/6kV to 12/20kV
Mining, drilling, and tunnelling cables represent the most demanding category of industrial cables, designed to operate in some of the harshest environments on earth. These heavy-duty power, control, and instrumentation cables serve mine operators worldwide for both static infrastructure and dynamic equipment applications. Manufactured in accordance with international standards including IEC 60502, BS EN 60332, BS EN 60811, BS EN 60754, and VDE 0295, mining cables must withstand mechanical stress, oil and grease exposure, water immersion, and in underground applications, provide critical fire safety through reduced smoke and fume emissions.

What are Mining, Drilling & Tunnelling Cables?

NSSHÖU cable, NSSHOU cable, NSHÖU cable, NSHOU cable, NSSCHOU cable, NSHTÖU cable, NTSCGEWÖU cable, NTSCGEWOU cable, NTMCGEWÖU cable, N3GHSSYCY cable, N3GHSSHCH cable,Type 61 cable, Type 63 cable, Type 611 cable, Type 622 cable, Type 633 cable, Type 66 cable,Type 240 cable, Type 241 cable, Type 245 cable, Type 450 cable, Type 455 cable, Type 260 cable, Type 275 cable, Type 409 cable, Type 440 cable, Type 441 cable,
BS6708, mining cable, quarry cable, trailing cable, EPR cable, SWA cable, coal cutter cable, excavator cable, 礦用電纜, 採石場電纜, 拖曳電纜

What is BS6708 Cable?

British Standard BS6708 sets out the requirements for flexible trailing cables where used in mining operations and quarries. These cables are often referred to as trailing cables, quarry cables, or auxiliary cables and have applications with a wide range of dynamic mining equipment including excavators, coal-cutters, crushing machines, and shuttle cars. flexible trailing cable, mine cable, EPR mining cable, SWA mining cable, chloroprene cable, coal cutter cable, excavator cable, shuttle car cable, crushing machine cable, coal face cable, Type 7 mining cable, Type 7M cable, Type 7S cable, Type 11 cable, Type 20 cable, Type 21 cable, Type 307 cable, Type 331 cable, Type 621 cable, Type 631 cable, 640/1100V mining cable, 1.9/3.3kV mining cable
Reeling Drum Cables for Port Cranes and Material Handling: Complete Engineering Guide Understanding NSHTÖU, TSCGEWÖU, and PUR Polyurethane Cables - Technical Specifications, Standards Compliance, Selection Criteria, and GB/T 5013 Limitations

Reeling Drum Cables for Port Cranes and Material Handling: Complete Engineering Guide

Reeling Drum Cables for Port Cranes and Material Handling: Complete Engineering Guide Understanding NSHTÖU, TSCGEWÖU, and PUR Polyurethane Cables – Technical Specifications, Standards Compliance, Selection Criteria, and GB/T 5013 Limitations
heavy-duty rubber cables represent a critical category for applications requiring exceptional mechanical strength, flexibility, and environmental resistance. This comprehensive technical guide examines three closely related cable types that dominate international markets for portable power transmission: the Chinese standard GB/T 5013 YC (Heavy-Duty General Rubber Cable) rated at 450/750V, the enhanced YCW variant with oil and weather resistance, and the European harmonized H07RN-F cable that serves as the international equivalent.

GB/T 5013 YC & YCW Heavy-Duty Rubber Cables and H07RN-F: Comprehensive Technical Analysis

heavy-duty rubber cables represent a critical category for applications requiring exceptional mechanical strength, flexibility, and environmental resistance. This comprehensive technical guide examines three closely related cable types that dominate international markets for portable power transmission: the Chinese standard GB/T 5013 YC (Heavy-Duty General Rubber Cable) rated at 450/750V, the enhanced YCW variant with oil and weather resistance, and the European harmonized H07RN-F cable that serves as the international equivalent.
What is PROTOMONT NSSHOEU 1 kV Low Voltage Flexible Rubber Cable? A Comprehensive Technical Guide to Heavy-Duty Mining and Industrial Flexible Cables with EPR Insulation for Extreme Environments

What is PROTOMONT NSSHOEU 1 kV Low Voltage Flexible Rubber Cable?

PROTOMONT NSSHOEU series represents a category of heavy-duty, low voltage flexible rubber cables engineered specifically for demanding industrial environments. These cables are designed to provide reliable power transmission in applications where conventional cables would fail due to extreme mechanical stress, environmental exposure, or chemical contact. The designation NSSHOEU follows German cable nomenclature standards where each letter indicates specific construction characteristics. The cables are manufactured according to DIN VDE 0250-812 specifications, which define requirements for rubber-insulated flexible cables used in power installations. According to industry standards, these cables are engineered for environments where high levels of mechanical stress and abrasion are expected, making them essential for modern mining, construction, and industrial operations.
PROTOLON(M) R-(N)TSCGEWOEU FO represents a sophisticated engineering solution that combines medium voltage power transmission with integrated fiber-optic communication capabilities in a single cable design. This innovative reeling cable is specifically engineered for demanding industrial applications where large mobile equipment requires simultaneous electrical power supply and high-speed data transmission under extreme mechanical stress conditions. The cable is manufactured according to the stringent requirements of DIN VDE 0250-813 standard, which is recognized globally as the definitive specification for flexible trailing cables used in heavy industrial applications.

What is PROTOLON(M) R-(N)TSCGEWOEU FO 6 kV – 35 kV Medium Voltage Reeling Cable with Integrated Fiber-Optics?

PROTOLON(M) R-(N)TSCGEWOEU FO represents a sophisticated engineering solution that combines medium voltage power transmission with integrated fiber-optic communication capabilities in a single cable design. This innovative reeling cable is specifically engineered for demanding industrial applications where large mobile equipment requires simultaneous electrical power supply and high-speed data transmission under extreme mechanical stress conditions. The cable is manufactured according to the stringent requirements of DIN VDE 0250-813 standard, which is recognized globally as the definitive specification for flexible trailing cables used in heavy industrial applications.
ANSI/NEMA WC 58 / ICEA S-75-381: Portable and Power Feeder Cables for Mining Applications

ANSI/NEMA WC 58 / ICEA S-75-381: Portable and Power Feeder Cables for Mining Applications

ANSI/NEMA WC 58 / ICEA S-75-381 standard represents one of the most comprehensive specifications for portable and power feeder cables used in mining environments. According to industry analysis, this standard represents one of the most rigorous cable specifications ever developed, specifically addressing the unique challenges encountered in both surface and underground mining operations where equipment reliability directly impacts production efficiency and worker safety.
What is TYPE 450 1.1 to 33kV Mining Cables to AS/NZS 2802:2000?

What is TYPE 450 1.1 to 33kV Mining Cables to AS/NZS 2802:2000?

TYPE 450 cables occupy a critical position within this standard as Class 2 cables, distinguished by their incorporation of semiconductive screening systems essential for medium to high voltage applications. The designation “Type 450” refers to the cable’s construction classification within AS/NZS 2802:2000, with the numeric suffix (450.3, 450.6, 450.11, 450.22, 450.33) indicating the voltage rating in kilovolts. These cables are specifically engineered for slow reeling and trailing applications where equipment such as draglines, excavators, and wharf cranes requires flexible power connections that can withstand thousands of reeling cycles while maintaining electrical integrity and mechanical reliability.
CEI 20-27 CENELEC HD361 Cable

What is CEI 20-27 CENELEC HD361 Cable?

CEI 20-27 CENELEC HD361 represents a standardized cable designation system developed by the European Committee for Electrotechnical Standardisation (CENELEC) to provide uniform identification and classification of harmonized power cables and cords across European markets. This systematic coding methodology enables engineers, procurement specialists, and electrical contractors to precisely identify cable specifications including voltage ratings, insulation materials, conductor types, and sheathing compounds through a structured alphanumeric designation format.